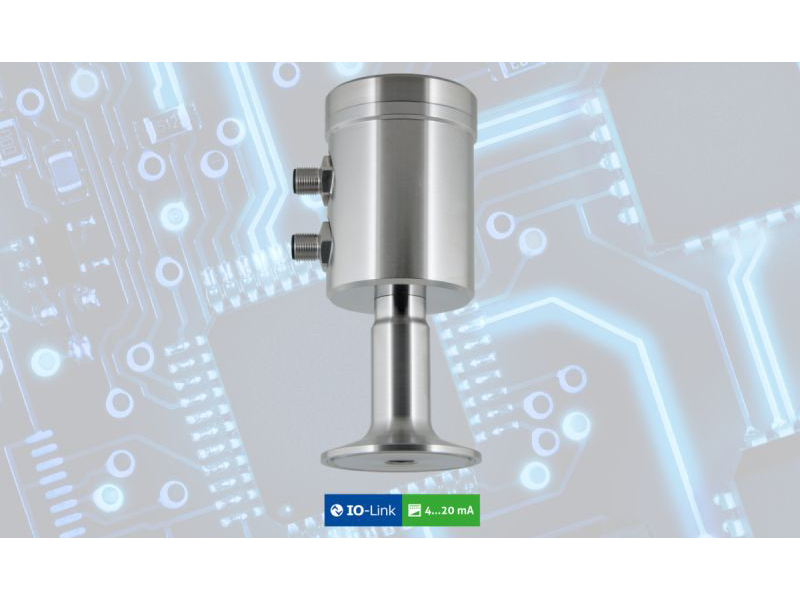
The Anderson-Negele ITM-51 Backscatter Turbidity Sensor is designed to enable active, automated phase-transition control, eliminating reliance on passive time or volume-based switching.
By measuring turbidity in real time, the ITM-51 reduces unnecessary product losses, shortens process cycles, and improves overall plant efficiency.
Key application areas:
- CIP systems – monitoring contamination levels of rinse and cleaning media with automatic switch-over to re-use or discharge
- Separator and cooler control
- Yeast harvesting
- Inline product quality monitoring
Technical advantages:
- Compact design with clamp or screw process connections
- Flush, hygienic inline integration
- Extended measurement range: 200 to 300,000 NTU
- Accuracy up to ±3%, repeatability <1%
- High cost-saving potential — ROI often achieved within weeks
The ITM-51 provides measurable efficiency gains by ensuring media transitions occur precisely when needed, not based on conservative time settings.
Raymond Karsten
Instek Control (Pty) Ltd
Tel. +27 12 998 6326
info@instek.co.za
www.instek.co.za